
TL;DR: Position the clamp so the plunger engages the workpiece in roughly the last 10-15% of its downward arc, mark and drill through the base itself (not a template), and secure with 1/4-20 machine screws into T-nuts or threaded inserts. Wood screws into MDF will fail. Dry-fit before you reach for the Loctite.
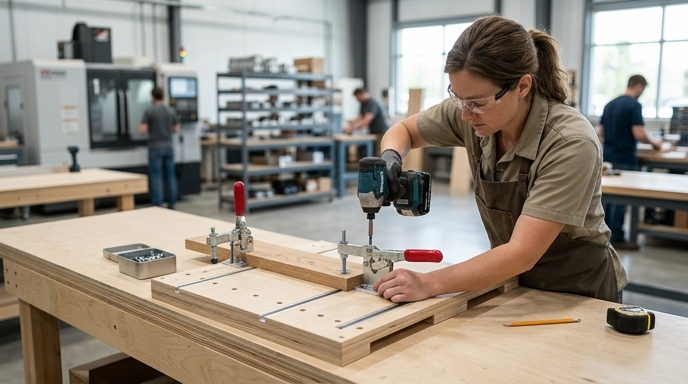
Choosing the Right Clamp Before You Drill a Single Hole
Match the clamp to the job. A drill press stop block needs almost nothing. A router template fighting bit climb on figured maple needs real pressure, and the fasteners that go with it.
The industry-standard clamps were popularized by De-Sta-Co and have since been cloned by Powertec, Harbor Freight’s Bremen line, and a dozen Amazon brands you’ve probably never heard of. They’re categorized by holding capacity. The De-Sta-Co 202-U gives you 200 lbs, which is fine for light hold-downs. The 207-U (and its Powertec equivalent, the 20501) delivers 375 lbs and is what most people end up on for table saw sleds and pocket-hole jigs. The 210-U steps up to 600 lbs for CNC fixtures and heavier routing.
One thing people overlook: the 210-U has a mounting footprint around 1.75 x 1.25 inches, which will overhang a narrow fence. Check the spindle length against your thickest workpiece, too.
| Clamp Model (De-Sta-Co / Powertec) | Holding Force | Common Application |
|---|---|---|
| 202-U / 20301 | 200 lbs | Drill press stops, light assembly jigs |
| 207-U / 20501 | 375 lbs | Table saw sleds, router templates |
| 210-U / 20320 | 600 lbs | CNC hold-downs, heavy milling |
Mapping Over-Center Geometry (The Step Everyone Skips)
A toggle clamp locks because the internal linkage physically passes its pivot point in the last stretch of the handle’s travel. For most vertical clamps that engagement zone sits in the final 10-15% of the arc. If the linkage doesn’t cross center, the clamp doesn’t lock. Simple as that.
Mount the base too close to the workpiece and the rubber plunger hits wood too early. The handle fights you and never crosses over. Mount it too far back and the handle locks fine but the plunger does nothing — you’ve built a very satisfying piece of theater that applies no downward force.
Here’s how to find the setback before you drill anything. Put your actual workpiece on the jig. Thread the spindle down to roughly its midpoint. Press the handle until it clicks into the locked, over-center position. Then slide the whole clamp forward until the rubber tip firmly compresses the workpiece. That’s your mounting location. Mark it with a pencil before anything moves.
I know some folks eyeball this and get away with it on a short-handle 202-U. On a 210-U with a longer handle and more mechanical advantage, eyeballing it is how you crack a jig.
Fastener Selection by Substrate
The strongest mount uses 1/4-20 machine screws threaded into T-nuts recessed on the underside of the jig base. Every time you lock the clamp, the base wants to pull upward. Wood screws driven into MDF don’t care about your feelings, and they will eventually walk out.
Substrate matters a lot. Baltic birch holds T-nuts beautifully, probably because the cross-grain plies grab the prongs from every direction. Standard 3/4-inch MDF, on the other hand, tends to split or let the T-nut flange pull straight through under tension. Shop-built jig threads on r/woodworking are full of this complaint, and anecdotally it’s the single most common failure mode for first-time clamp installs. If you’re stuck with MDF, back up the T-nut with a steel washer on the underside, or just skip the T-nut entirely and run a through-bolt with a fender washer and a nyloc.
For solid hardwood jigs, zinc die-cast knife-thread inserts (E-Z Lok makes the ones I keep in the drawer) hold up well. Use pan-head or socket-cap screws. Flat-head countersunk screws will crack the stamped steel base if you lean on them, which you will, because that’s what people do with countersunk screws.
| Substrate | Recommended Fastener | Min. Thickness |
|---|---|---|
| Baltic Birch Plywood | 1/4-20 Machine Screw + 4-Prong T-nut | 1/2 inch |
| MDF | Through-bolt + Fender Washer + Nyloc Nut | 3/4 inch |
| Solid Hardwood | 1/4-20 Machine Screw + Threaded Insert | 3/4 inch |
Marking, Drilling, and Dry-Fitting
Don’t use a paper template. Stamped steel bases have enough manufacturing slop that a template drilled from spec sheets will put you off by a sixteenth, and now your screws are binding or your base is cocked.
Use the clamp itself. Position it per the over-center method above, hold it down with a small F-style bar clamp, and mark the dead center of each mounting hole with a transfer punch or a brad-point that matches the slot diameter.
For 1/4-20 T-nuts you want a 5/16-inch through-hole for the barrel. Flip the jig, drill a shallow 1/16-inch counterbore with a 3/4-inch Forstner over each hole so the T-nut sits flush and the jig lies flat on the bench. Seat the T-nuts with a hammer. Then dry-fit the whole thing and run a clamping cycle on scrap before anything gets Loctite.
The counterbore step is the one people skip and then complain about a wobbly jig.
Height Compensation When the Plunger Doesn’t Reach
If the plunger can’t reach the workpiece, raise the whole clamp. Do not just thread the spindle out further.
A long spindle acts as a lever against the base. You lose holding force, you multiply stress on the fasteners, and the stamped steel arm starts to flex noticeably on the heavier models. Keep the spindle threaded close to the arm.
For a riser block:
- Cut Baltic birch (or machine aluminum if you’re feeling fancy) to the clamp’s base footprint.
- Height it so the arm sits roughly parallel to the workpiece when locked.
- Drill 5/16-inch clearance holes all the way through the riser and the jig base.
- Run longer 1/4-20 machine screws through the clamp, the riser, and into the T-nuts underneath.
Locking the Install Against Vibration
Table saw sleds and router jigs generate the kind of high-frequency buzz that walks machine screws loose in a couple dozen cycles.
A drop of Loctite 242 (Blue) on the threads before final assembly handles this. Fixture time is 5-10 minutes, full cure 24 hours. If you’re through-bolting instead of using T-nuts, skip the Loctite and use nyloc nuts — they do the same job and you can disassemble later without heat.
Hand-tight on the 1/4-20s. Do not reach for the impact driver. You’ll crush wood fibers under the base, the clamp will cock slightly, and you’ve just permanently deformed your jig for no gain in holding power.
Retrofit Installations Where You Can’t Access the Underside
Sometimes you’re adding a clamp to a glued-up torsion box or a thick CNC spoilboard and the underside is simply not available. Threaded inserts are your only play.
Drill the pilot per the insert spec (typically 3/8-inch or 13/32-inch for 1/4-20, depending on wood density — the E-Z Lok datasheet will tell you). Drive from the top. On MDF or softwood, put a drop of CA or two-part epoxy on the external threads before driving the insert, or it’ll back out the first time you lock the clamp hard.
One honest warning: if the base is thinner than 3/4-inch and you can’t get underneath, the retrofit will probably fail. A 375-lb clamp will rip inserts out of 1/2-inch ply, epoxy or not. At that point you either rebuild the base or glue a 3/4-inch mounting block to the top surface and set the inserts into that.
Testing, Dialing In, and Common Install Failures
Once the Loctite has cured, run a real clamping cycle with the actual workpiece. The handle should push down with firm resistance and snap into the locked position. Tap the workpiece lightly with a mallet; it shouldn’t shift.
If something’s off:
- Handle won’t lock, or needs two hands. Base is too close, or spindle is threaded too far down. Back the spindle off first — it’s free. If that doesn’t fix it, relocate the base.
- Handle locks easy but the work slides. Opposite problem. Thread the spindle down. If it bottoms out before it bites, move the base closer.
- Back of the base lifts off the jig when locked. Your fasteners are losing the fight. This almost always means wood screws in MDF. Replace with through-bolts or T-nuts and don’t look back.
I’ll still spec a 207-U for a sled that probably only needs a 202-U, because I’ve been burned once and I’d rather have the extra margin than redo the install. That’s not a technical recommendation. It’s just how I do it.
FAQ
Can I mount a toggle clamp directly to MDF with wood screws?
No. The clamp pulls upward every time you lock it, and wood screws in MDF will strip within a few dozen cycles — sometimes within one if you really lean on it. Use machine screws into T-nuts, or through-bolt with fender washers. If MDF is all you have and you’re through-bolting, add a nyloc on the underside and you’ll be fine for most work.
How do I know if my toggle clamp is positioned correctly?
The rubber plunger should make firm contact with the workpiece just as the handle enters the last 10-15% of its downward travel, letting the linkage snap over-center.
What’s the strongest way to mount a toggle clamp?
1/4-20 pan-head machine screws through the base, into 4-prong steel T-nuts recessed into the underside of a Baltic birch or solid hardwood jig.
How much weight can a vertical toggle clamp hold?
Depends on the model. 202-U class: 200 lbs. 207-U / Powertec 20501 class: 375 lbs. 210-U class: 600 lbs.
