
Toggle clamps lock workpieces in place using an over-center linkage that turns a short handle motion into real clamping force. Four main types (horizontal, vertical, push-pull, and latch) cover almost everything you’ll run into in a workshop. The failure I see most often has nothing to do with the clamp itself. People bolt a 500-lb clamp onto an undersized base and the substrate flexes before the clamp ever reaches its rated capacity.
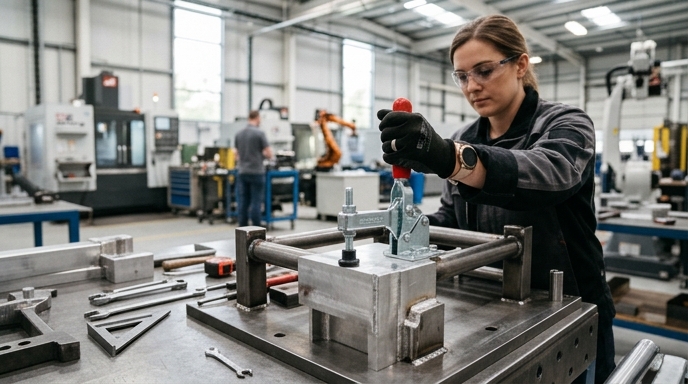
The Over-Center Mechanism: Why Toggle Clamps Lock Themselves
A toggle clamp works on a geometric trick called over-center linkage. There are three pivot pins. When you push the handle, those three pins briefly line up straight — that’s “dead center.”
Keep pushing and the middle pivot travels a few degrees past that line, and the linkage slams into a positive stop machined into the body. From that point on, any reverse pressure from the workpiece actually drives the linkage harder against the stop instead of pushing the handle open. No continuous hand pressure, no spring, nothing. It just sits there locked until you pull it back across dead center.
The over-travel is usually only a few degrees of rotation. That tiny bit of geometry is doing all the work.
The Four Clamp Families and When Each One Wins
Toggle clamps fall into four categories based on handle motion and clamping direction.
Horizontal Handle Clamps
The handle sits parallel to the bench when locked, which keeps your hand and the handle itself out of the way of cutting tools. The Destaco 225-U is the one most people have used at some point — 500 lb holding capacity, U-bar spindle. Standard choice for router sleds and CNC spoilboards where you don’t have overhead clearance to spare.
Vertical Handle Clamps
Handle stands up perpendicular to the bench when locked. You can pack more of them onto a single fixture because the footprint is tighter. The Destaco 207-U gives you 375 lbs and takes less horizontal real estate than a horizontal-handle equivalent. Drill press jigs are their natural habitat.
Push-Pull (Straight-Line) Clamps
The plunger moves in a straight line along its own axis instead of swinging through an arc. The Destaco 604 pushes forward to lock at 300 lbs. Woodworkers reach for these for drawer-front gluing and edge banding, anywhere you need lateral pressure instead of top-down hold.
Latch-Action (Pull-Action) Clamps
A U-bolt or J-hook reaches out, catches a latch plate, and pulls it in. The Destaco 331 is rated at 700 lbs. Mold halves, pressure vessel lids, custom toolbox closures — anywhere two things need to be yanked together and held.
| Type | Handle Motion | Typical Force Range | Best For | Worst For |
|---|---|---|---|---|
| Horizontal | Parallel to base | 100 – 1,000 lbs | Router sleds, CNC beds | Deep, narrow jigs |
| Vertical | Perpendicular to base | 100 – 1,000 lbs | Drill press tables | Low-clearance setups |
| Push-Pull | Linear (in/out) | 100 – 16,000 lbs | Edge gluing, lateral stops | Top-down hold-downs |
| Latch | Pulling arc | 300 – 7,500 lbs | Molds, lids, doors | Flat sheet goods |
Reading a Spec Sheet Without Getting Fooled
Manufacturers list two different numbers on toggle clamp spec sheets, and people mix them up constantly. Holding capacity and clamping force are not the same thing.
Holding capacity is the maximum static load the locked clamp can resist before the frame yields or permanently deforms. A 500 lb holding capacity means 501 lbs of upward force from the workpiece is going to bend an arm or shear a rivet.
Clamping force is the actual downward pressure the spindle tip puts on the workpiece. This number is always lower than the holding capacity, sometimes by a lot. The ratio between the two depends on the clamp’s internal mechanical advantage and, critically, where you set the spindle on the U-bar. Spindle closer to the base, more clamping force. Spindle out at the far end of the bar, less force, because you’ve increased the leverage against yourself.
Standard engineering practice is a 3:1 or 4:1 safety factor for manual workholding. If your cut is throwing 100 lbs of lift at the part, you want a clamp rated 300 to 400 lbs minimum. I run closer to 4:1 for anything with interrupted cuts, which I’ll admit is probably more conservative than it needs to be. Old habit from a job where a part came loose on a shaper and that was the end of that discussion.
Mounting Done Right — Substrate, Bolts, and Reinforcement
A 500 lb toggle clamp bolted to a weak base will fail at 50 lbs of load. The substrate just flexes, the clamp never reaches its over-center position, and you spend an afternoon trying to figure out why your “500 lb” clamp isn’t holding.
For wood jigs, 3/4-inch Baltic birch or 3/4-inch MDF is the floor for clamps up to about 300 lbs. For 500 lbs and up, laminate two layers of 3/4″ or just use an aluminum fixture plate and stop fighting it. Flanged bases spread the load wider than straight bases, which is why they’re standard for flat-surface mounting.
Don’t use wood screws. Not for anything that’s going to see machining loads. The threads strip, usually at the worst possible moment.
Step-by-Step Mounting Checklist:
- Mark the four hole locations using the clamp base as a template.
- Drill through-holes sized for 1/4-20 machine bolts (for standard 200–500 lb clamps).
- Insert the 1/4-20 bolts from the top down.
- Place a steel backing plate or wide fender washers on the underside of the jig.
- Secure with nylon-insert lock nuts so vibration doesn’t walk them loose.
Fender washers are the lazy version of a backing plate. They work, mostly. A proper piece of 1/8″ steel bar across the back of the mounting pattern is better and takes an extra ten minutes.
Dialing In Clamping Force with the Spindle Adjustment
The spindle is the threaded rod with the rubber tip that actually touches the workpiece. Most standard spindles come with a neoprene tip around 85 Shore A, which grips without marring.
Set the spindle wrong and you get one of two problems. Too tight: you’re slamming the handle down, crushing the part, and chewing up the pivot pins. Too loose: the part slips mid-cut.
The 10-Second Calibration Method:
Put the actual workpiece under the clamp. Close the handle all the way into locked position. Back the spindle nuts off until the threaded rod moves freely. Spin the spindle down by hand until the neoprene tip just kisses the workpiece. Open the handle. Turn the spindle down exactly one-quarter turn. Tighten the jam nuts. Close the clamp. It should snap in with firm, moderate resistance — the kind of resistance where you know it’s locked but you’re not throwing your shoulder into it. If it slips, add another quarter turn.
Real Failure Modes (and How to Prevent Them)
Toggle clamps fail in predictable ways.
Handle whip-back is the one that’ll get you hurt. When an over-tightened clamp releases, the stored energy in the compressed neoprene tip throws the handle open hard and fast. OSHA’s general machine guarding standard (1910.212) covers pinch-point planning in broad strokes; practically, keep your hand out of the handle’s upward swing arc on release. I’ve got a scar on the web of my left thumb that explains this better than any paragraph can.
Vibration loosening happens on heavy milling or routing work. The chatter travels through the jig and backs the spindle jam nuts off a fraction of a turn per cycle until suddenly the spindle’s a quarter inch low. Machinists fix this with blue Loctite (242) on the spindle threads after calibration, or they double-nut it. Either works. I prefer double jam nuts because you can adjust without waiting for anything to cure.
Neoprene compression set is the slow one. Leave a clamp locked on a workpiece for a few weeks and the rubber tip flattens permanently. Loses its elasticity, loses its grip. Store them open.
Jig and Fixture Design Patterns That Actually Work
Clamp placement is most of the game. The clamping force always needs to push the workpiece into a solid hard stop or fence. Never set a clamp up where its primary vector pushes the material into open space and you’re hoping the rubber tip’s friction holds it. That’s not holding, that’s praying.
Multiple small clamps beat one big clamp almost every time. Four 200-lb clamps spread along a workpiece give you even pressure, no bowing. One 800-lb clamp dead center and the ends of the part lift off the fixture plate like a seesaw.
Map the handle swing before you drill mounting holes. The classic rookie move: vertical toggle clamp set up a hair too close to a router template, and when it’s locked the handle blocks the router base from passing over the part. Now you’re drilling new holes.
When Toggle Clamps Are the Wrong Tool
Toggle clamps have limits.
Anything above about 1,000 lbf of required clamping force, you’re into hydraulic or pneumatic territory. Manual clamps in that range need handles too long to be practical on a benchtop.
High-vibration operations — aggressive fly-cutting on a manual mill is the usual culprit — can bounce the over-center mechanism open. Threaded screw clamps or cam-action clamps are a more secure mechanical lock in those situations because there’s nothing to shake past dead center.
Variable part thickness is the other dealbreaker. If your parts vary more than 1/16″ piece-to-piece, you’re going to be recalibrating the spindle constantly, and nobody actually does that, which means parts come out wrong. Auto-adjusting clamps like the Bessey STC series use an internal spring to accommodate thickness variation up to 1-1/4″ while keeping clamping pressure constant. They cost more. They’re worth it on any production run where you’re not sorting parts to thickness first.
FAQ
How much weight can a toggle clamp actually hold?
Holding capacities span from about 50 lbs on miniature instrument clamps up to 16,000 lbs on heavy-duty forged models. But the real answer is: however much your mounting setup can take. The clamp is almost never the weak link.
Can I use a toggle clamp upside down or sideways?
Yes. The lock is geometric, not gravitational. Walls, under tables, compound angles — doesn’t matter.
Why does my toggle clamp handle feel loose or sloppy?
Worn pivot pins or stretched rivet holes. It happens when the clamp has been chronically over-tightened, so the linkage is carrying loads past its rating every cycle. Once the rivets stretch, the clamp can’t hold a clean dead-center lock anymore and you’re not fixing it. Replace it.
Do I need to lubricate toggle clamps?
A few drops of light machine oil (ISO VG 32 or 46) on the pivot pins every 300 to 500 cycles. That’s the manufacturer line and it’s about right. Keeps the rivets from galling and the handle feel stays consistent for years instead of months.
